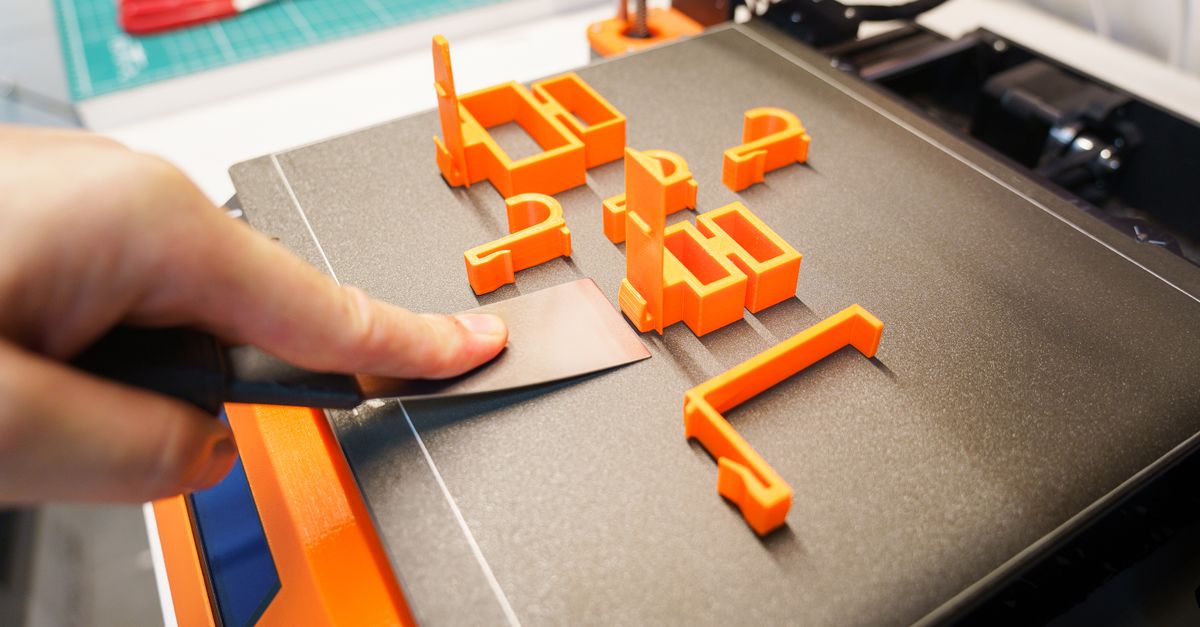
Photo by Jakub Zerdzicki on Pexels
Reverse Engineering Broken Parts for 3D Printing
Every maintenance manager, restorer, and equipment owner eventually meets the same problem: a small part fails, the manufacturer no longer makes it, and there is no drawing anywhere. Reverse engineering parts for 3D printing is how you get out of that corner. You take a physical part (even a cracked or worn one), turn it into a clean digital model, and print a working replacement. Done well, it is one of the most practical uses of FDM technology. Done carelessly, it produces a part that looks right and fails in a week.
This guide walks through how the process works, what to capture, and where most people go wrong.
Why Reverse Engineer Instead of Just Copying the Part?
A worn part is not the original design. If you scan or measure a bracket that has been in service for 15 years, you are measuring a part that has been deformed, worn, and possibly repaired. Copying those dimensions faithfully gives you a faithfully worn replacement. Reverse engineering means understanding design intent: what the part was supposed to do, which surfaces mate with something else, and which features are incidental.
The goal is a better model, not a mirror image. The original may have been injection molded, cast, or machined. Those processes impose constraints (draft angles, casting radii, tool access) that do not apply to FDM. A good reconstruction keeps the functional geometry and adapts everything else to suit layer-by-layer printing.
How Do You Capture the Geometry?
There are three common approaches, and many real projects combine them.
Manual measurement
Digital calipers, micrometers, pin gauges, and radius gauges handle a surprising share of parts. For brackets, housings, spacers, knobs, clips, and covers, a good set of measurements plus photos is often all you need. Calipers typically resolve to 0.01 mm, which is far finer than the process we print with, so the limiting factor is how carefully the part is measured and how well its features are understood.
Manual measurement works best when the part is mostly prismatic: flat faces, round holes, simple bosses. It becomes slow and error-prone with organic curves or compound angles.
3D scanning
Structured-light and laser scanners capture surface geometry as a mesh or point cloud. Accuracy varies widely by equipment, from roughly 0.02 mm for professional metrology scanners to 0.1 mm or more for lower-cost handheld units, and photogrammetry from phone photos is coarser still. Shiny, dark, or transparent surfaces often need a matte developer spray to scan well.
Scan data is a starting point, not a finished model. A raw mesh is noisy, has holes, and carries every scratch and burr. It usually has to be converted into clean CAD geometry before it is useful for revision or production. If you already have scan data, our guide to 3D printing file formats explains which formats are practical to work from.
Reference parts and drawings
Sometimes you have a mating part, a photo with a known dimension, or an old hand-sketched drawing. Mating components are valuable because they define the real interface dimensions, which matter more than the dimensions of the broken part itself.
Photo by Jakub Zerdzicki on Pexels
What Should You Document Before Modeling?
Identify the critical features first. Separate the surfaces that must be precise (bearing seats, mounting hole spacing, sealing faces, snap features) from the ones that are cosmetic. This decides where to spend your effort and where tolerance can be relaxed.
Record the operating conditions. Temperature, load direction, chemical exposure, UV, vibration, and duty cycle all drive material choice. A part that sits under a car hood faces very different conditions than one inside an office enclosure.
Note how the original failed. A cracked mounting ear tells you the original was under-designed or overloaded, and a replacement that copies it exactly will crack in the same place. Failure mode is design information. It tells you where to add material, increase a fillet radius, or change print orientation.
Capture the mating hardware. Bolt sizes, thread types, bearing dimensions, and clearances to neighboring parts all belong in your notes. If you are designing around heat-set hardware, see our post on heat-set inserts.
How Do You Adapt the Model for FDM Printing?
This is where reverse engineering becomes engineering rather than tracing.
Compensate for the process. FDM holes tend to print slightly undersized, often by 0.1 to 0.3 mm depending on diameter, orientation, and settings. Shafts and pins can print slightly oversize. Press-fit and sliding interfaces need deliberate offsets in the CAD model, then a test print to confirm. Our overview of 3D printing tolerances covers realistic expectations in detail, and tolerance stackup matters if the part is one of several in an assembly.
Design for the load path. FDM parts are weakest between layers. If the original part was machined from solid aluminum, it has the same strength in every direction. A printed version does not. Orient the part so that primary loads run along the layers rather than pulling them apart, and add wall thickness where stress concentrates. See part orientation and infill vs walls for how those choices affect strength.
Add what the original lacked. Larger fillets at stress points, ribs, integrated bosses for heat-set inserts, or consolidated features can all make the replacement better than the original. This is also where part consolidation can pay off, since an assembly of three stamped pieces might become a single printed part.
Remove what you do not need. Draft angles, mold parting lines, casting bosses, and machining reliefs can often be dropped or simplified.
Which Material Should Replace the Original?
Material selection is the step most often rushed. A few general guidelines:
- PLA is rigid, easy to print, and dimensionally accurate, but softens at roughly 55 to 60 C. It suits fixtures, display pieces, and indoor low-temperature use.
- PETG offers better toughness, chemical resistance, and moderate heat tolerance. It is a strong default for functional replacement parts, and one of the two materials we print daily.
- ABS and ASA step up in heat resistance, and ASA adds UV stability for outdoor exposure. We run ABS periodically and can print ASA when a project calls for it.
- Nylon, TPU, and carbon fiber composites cover specialized needs like wear resistance, flexibility, and stiffness. We can print these, though they are not our everyday materials.
If the original is metal, the question is whether plastic can carry the load at all. Our metal-to-plastic conversion guide covers how to decide, and PLA vs PETG vs ABS is a helpful comparison for the most common choices.
How Do You Validate the Replacement?
Print a test fit first. Before committing to a final material and a full quantity, print a quick draft in a low-cost material to check hole spacing, clearances, and assembly. This is classic rapid prototyping logic: iterating on a cheap print is far less costly than discovering an error on the final part.
Check critical dimensions on the print. Measure the features you flagged as critical. A simple go/no-go gauge or the mating hardware itself often works. For production runs, the approach in first-article inspection gives you a structured way to approve the first part before printing the rest.
Test under real conditions. If the part sees heat, vibration, or load, test it in that environment before you rely on it. Safety-critical components deserve extra caution, and some should not be replaced with printed parts at all without proper engineering review.
Save everything. Keep the final CAD, the measurements, the print settings, and the revision history together. Version control for print files makes it easy to reprint the same part next year without starting over.
What About Intellectual Property?
Reverse engineering for repair and maintenance of equipment you own is common practice, but some parts are protected by patents, design registrations, or contractual terms. Replicating a part for your own repair is generally treated differently from producing and selling copies. This is not legal advice, and if you plan to produce parts commercially, it is worth confirming your position with an attorney.
Where Does This Approach Pay Off Most?
Reverse engineering delivers the best return in situations where the part is low-volume, hard to source, or costly to wait for:
- Classic and vintage vehicles, where trim pieces, brackets, and interior components have been out of production for decades. See 3D printing for classic car restoration and our automotive restoration service.
- Legacy equipment, where a plastic knob, guard, or bracket is holding up a machine that otherwise works fine. The spare parts inventory approach of storing digital files instead of shelves of parts fits naturally here.
- Shop floor fixtures and tooling, where a lost or damaged jig needs to be recreated. Our manufacturing tooling and fixtures service covers this kind of work.
- Small production runs, where a reconstructed part is needed in quantities of 10 to a few hundred. That is the territory of small-batch production.
Start With the Part in Your Hand
You do not need a finished CAD file, or even a drawing, to get started. A physical sample, a few photos, and a clear description of how the part is used give a designer enough to begin. If you are not sure how to handle the modeling step, our custom design services exist for exactly that situation, and the post on working without a CAD file explains what the process looks like.
Ready to Rebuild a Part That Cannot Be Bought?
If you have a worn, broken, or discontinued part and want to know whether a 3D printed replacement is realistic, tell us about it. Send photos, dimensions, and a note about where the part is used, and we will help you work out the material, the design changes, and the best path to a working replacement.
Start your project at /custom-order
Related Reading
Related Articles
Creep in 3D Printed Parts: Why Plastic Sags
Creep in 3D printed parts is slow deformation under constant load. Learn which materials resist it and how to design parts that keep their shape.
Designing Snap Fits for FDM 3D Printing
Snap-fit design for FDM comes down to strain, orientation, and clearance. Here is how to build snap fits in PLA and PETG that do not crack.
Infill vs Walls: What Makes 3D Prints Strong
3D print strength depends more on walls, orientation, and material than on infill percentage. Here is how to spec parts that hold up without overpaying.